How to Ensure Bottle Quality During Shipping from China?

Time:2026-09-20 Author:Henry
0%

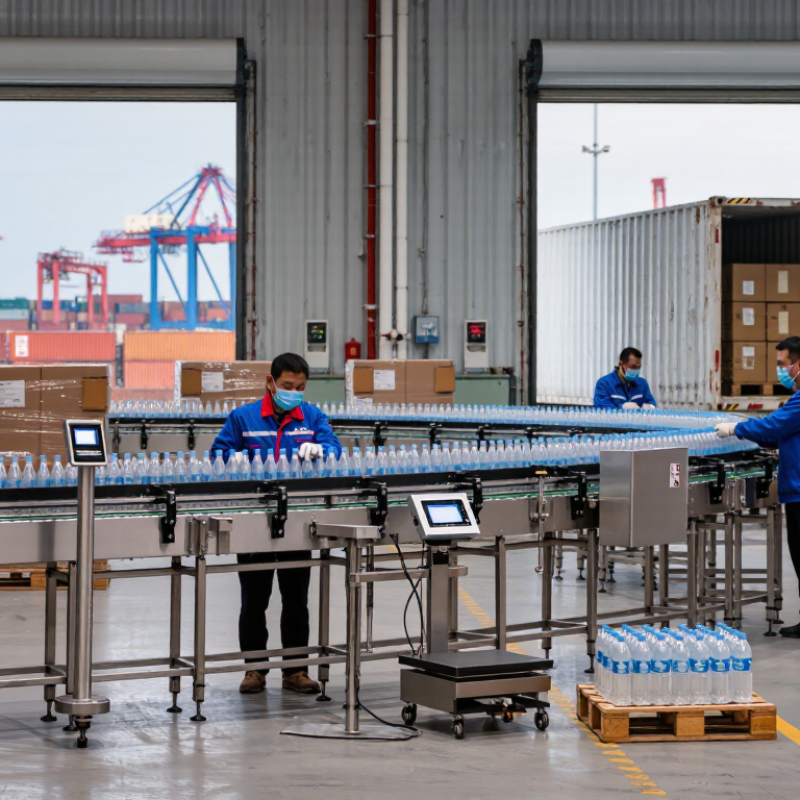
How to ensure bottle quality during shipping is a practical question for every China-based packaging project. Bottles may leave a clean factory in Guangdong, yet arrive with scuffs, cracked necks, loose caps, or distorted labels. The journey matters. UNCTAD’s Review of Maritime Transport reports that more than 80% of global merchandise trade by volume moves by sea. That exposure can mean weeks of vibration, container movement, humidity, and temperature changes before delivery.

A reliable quality plan should connect factory controls with transport testing. Inspect bottle dimensions, wall thickness, closure torque, surface finish, and carton strength before loading. Keep dated inspection records and retain production samples. ISTA 3A testing is useful because it simulates common parcel hazards, including impact, compression, and vibration. For palletized ocean freight, teams should also review container loading patterns, corner protection, moisture barriers, and internal movement. The World Bank’s Logistics Performance Index 2023 highlights differences in infrastructure, shipment reliability, and logistics competence across markets. Those differences can affect delivery conditions, even when the supplier performs well.

Real shipments are messier. A perfect factory sample proves little if cartons shift inside the container. This is where experience becomes valuable: photograph pallet conditions, measure humidity when needed, and compare arrival defects with pre-shipment records. Do not rely on packaging appearance alone. A stronger approach combines supplier audits, sampling inspections, ISTA-informed testing, and clear acceptance criteria. Some risks remain difficult to predict, especially during peak seasons or transshipment. That limitation deserves attention, not denial. This guide explains how to ensure bottle quality during shipping through practical controls, evidence-based checks, and continuous review.
How to Ensure Bottle Quality During Shipping from China?

Define Bottle Quality Standards Before Production

How to Ensure Bottle Quality During Shipping from China?

Define Bottle Quality Standards Before Production

Bottle quality should be defined before a factory purchases materials or prepares molds. A vague phrase like “premium finish” invites inconsistent judgment. Create a signed specification sheet covering dimensions, capacity, wall thickness, weight, color, closure fit, leakage, and surface defects. Add clear limits for scratches, bubbles, dents, and print misalignment. Include photos of acceptable and rejected samples.

Transport conditions also require measurable standards. The 2023 Pitney Bowes Parcel Shipping Index recorded 161.1 billion parcels worldwide in 2022. That volume means bottles may face repeated handling, vibration, compression, and sudden drops. Specify packaging requirements before production. Request carton drop testing under ASTM D4169 or ISTA procedures. Test filled samples, not only empty bottles. Empty bottles behave differently.

Use a pre-production sample and approve it in writing. Then inspect the first production batch against the same sample. Independent inspection can check dimensions, torque, leakage, visual quality, and carton strength. Use a documented sampling plan, such as ISO 2859-1, instead of relying on a few attractive pieces.

UNEP’s Global Waste Management Outlook 2024 projects municipal waste could reach 3.8 billion tonnes by 2050. Overpackaging is not automatically good quality. It may hide weak design and increase waste.

I have seen teams focus heavily on appearance and neglect closure performance. That mistake deserves review. Small details matter.

Select Reliable Materials and Inspect Manufacturing Processes

How to Ensure Bottle Quality During Shipping from China?

Bottle quality begins with material control, not container loading. Choose resin or glass with stable composition, documented batch numbers, and supplier certificates. For PET and HDPE bottles, verify wall thickness at the shoulder, base, and neck. Uneven walls often collapse during stacking. For glass, inspect for stones, bubbles, cracks, and sharp finish edges. The World Bank’s 2023 Logistics Performance Index scores China at 3.7 out of 5, showing strong logistics performance but uneven conditions across routes. Packaging must still tolerate delays, vibration, and temperature changes.

Tips: Request a pre-production sample. Approve a sealed golden sample. Check dimensions with calibrated gauges. Test closure torque and leakage. Use ISO 2859-1 sampling plans for consistent acceptance decisions. ASTM D4169 can guide vibration, compression, and drop testing. Do not rely on appearance alone. A clean bottle may still fail pressure testing.

During manufacturing inspections, review incoming materials, molding temperatures, cooling time, and machine settings. Inspect the first articles before mass production begins. Keep hourly records for weight, neck finish, color, and defects. A practical shipping trial should include pallet compression and edge-drop checks. Use dividers that prevent bottle-to-bottle contact. Control pallet height carefully. One overlooked risk is humidity inside containers; carton softening can reduce stacking strength. Factory reports may look complete, yet traceability gaps remain. That deserves correction before shipment. Randomly open packed cartons, photograph findings, and match them with batch records. Small inconsistencies become expensive after arrival.

How to Ensure Bottle Quality During Shipping from China? - Select Reliable Materials and Inspect Manufacturing Processes

Quality Dimension Inspection Point Recommended Acceptance Criteria Inspection Method and Timing Why It Matters During Shipping
Material Selection Glass composition Use container glass with a consistent composition and verified compatibility with the intended liquid. For repeated thermal changes, borosilicate glass may be considered where appropriate. Review material declarations and supplier documentation before production; confirm with sample testing. Incompatible or inconsistent glass can increase the risk of cracking when exposed to impact or temperature variation.
Material Selection Plastic resin identification Confirm the specified resin, such as PET, HDPE, or PP, matches the approved product specification and intended application. Check resin documentation, production records, and resin identification testing before mass production. The wrong resin may reduce strength, cause deformation, or create compatibility problems with the contents.
Material Selection Recycled content and additives Verify the declared recycled content, colorants, UV stabilizers, and other additives against the purchase specification and applicable regulations. Review batch records and declarations; perform laboratory verification when required by the product or market. Uncontrolled additives or inconsistent recycled content may affect clarity, brittleness, odor, and dimensional stability.
Manufacturing Process Wall thickness and distribution Measurements should remain within the approved drawing tolerance, with no thin areas that could compromise impact resistance or sealing performance. Measure samples at defined points using calibrated gauges or ultrasonic equipment during production and final inspection. Uneven walls can create weak zones that are more likely to crack, collapse, or deform under stacked loads.
Manufacturing Process Neck finish and thread accuracy The neck dimensions, thread profile, and sealing surface must match the approved drawing and closure specification. Use thread gauges, profile gauges, and closure fit checks on samples from each production batch. An inaccurate neck finish may cause loose caps, leakage, cross-threading, or damage during handling.
Manufacturing Process Sealing performance The bottle and closure combination should pass the approved leak test without visible leakage, cap displacement, or seal failure. Conduct vacuum, pressure, inversion, or dye-penetration testing according to the package design and product risk. A reliable seal protects the contents from leakage, contamination, and pressure changes during transport.
Appearance Surface defects No cracks, splits, sharp edges, severe scratches, black spots, foreign particles, bubbles, or other defects that affect function or safety. Perform visual inspection under controlled lighting using an approved defect sample board. Existing defects can expand under vibration, compression, and repeated impact during transit.
Dimensions Height, diameter, and capacity All critical dimensions and nominal capacity must remain within the tolerances stated on the approved technical drawing. Use calibrated calipers, height gauges, and volumetric checks during first-article and final inspections. Dimensional variation may cause unstable pallet stacking, poor carton fit, or excessive movement inside the package.
Mechanical Strength Top-load and compression resistance The bottle must withstand the specified compressive load without collapse, permanent deformation, or loss of seal. Conduct compression testing using a defined load, test speed, and holding time based on the packaging design. Insufficient compression strength can cause failures in lower carton layers during warehouse stacking and transport.
Mechanical Strength Drop and impact resistance Samples should meet the approved drop-test protocol without leakage, hazardous breakage, or unacceptable deformation. Test the filled bottle and shipping pack from specified heights and orientations representative of the distribution route. Impact testing helps identify failure risks caused by loading, unloading, sorting, and accidental drops.
Packaging Internal protection Dividers, trays, sleeves, or cushioning should prevent bottle-to-bottle contact and limit movement inside the carton. Inspect packaging assembly and conduct vibration or transport simulation with representative units. Controlled movement reduces abrasion, edge impact, glass-to-glass contact, and cap damage.
Packaging Carton strength and stacking The outer carton should support the planned stacking height and remain intact under expected humidity and handling conditions. Review carton board specifications and perform compression, vibration, and stacking tests where necessary. Weak cartons can collapse or lose protective geometry, exposing bottles to compression and impact damage.
Environmental Control Temperature and humidity exposure Define acceptable storage and transport conditions for the bottle material, closure, labels, and contents. Use route-specific environmental data or simulated conditioning before final packaging approval. Heat, cold, and humidity can cause plastic deformation, glass stress, adhesive failure, corrosion, or seal changes.
Inspection Control Sampling and inspection records Maintain traceable batch numbers, inspection results, test equipment details, defect counts, and corrective actions. Complete pre-production, during-production, and pre-shipment inspections using a documented sampling plan. Traceability allows damaged batches to be isolated and recurring manufacturing or packing problems to be corrected.
Final Release Pre-shipment approval Release only after all critical criteria pass; unresolved critical defects should prevent shipment. Compare inspection results with the approved specifications, packaging plan, and shipping marks before loading. A final release check reduces the probability of sending defective, unstable, or incorrectly packed bottles.

Use Protective Packaging to Prevent Damage During Transit

How to Ensure Bottle Quality During Shipping from China?

Protective packaging is the first quality check after production. In 2022, global parcel volume reached 161.8 billion shipments, according to the Pitney Bowes Parcel Shipping Index 2023. Bottles may face drops, vibration, stacking pressure, and temperature changes during this journey. A strong carton alone cannot prevent damage. Use molded pulp, foam inserts, or adjustable dividers to keep each bottle separated. Leave no space for bottles to move. For glass containers, add cushioning around the neck and base. These areas often fail first.

ISTA 3A testing evaluates common distribution hazards, including shock, vibration, compression, and environmental conditioning. Testing a packed sample before shipment can reveal weak points. A practical trial should include carton drops, repeated vibration, and stacking under weight. Check for hairline cracks, loose closures, label scuffing, and leakage. One weakness remains easy to miss: packaging that protects bottles may also increase shipping weight and cost.

Tips: Select a five-layer corrugated carton for heavier bottles. Wrap closures separately. Use moisture-resistant inner protection during humid seasons. Keep cartons on pallets, away from direct floor contact. Photograph the packing process for traceability. Do not rely on “fragile” labels alone; handling systems cannot guarantee special treatment. A smaller carton may reduce movement, but an over-tight fit can create pressure points. Test both options before full production.

Control Shipping Conditions and Track Product Handling

Bottle quality can decline long before a shipment reaches its destination. During export handling, cartons may face vibration, sudden braking, stacking pressure, humidity, and temperature changes. A reliable shipping plan should define acceptable conditions before loading begins. For example, glass bottles need firm separators, edge protection, and tested carton strength. Plastic bottles still require protection from deformation and heat.

Control begins with measurable details. Record the loading temperature, carton arrangement, pallet height, and seal condition. Use shock and tilt indicators when the route includes multiple transfers. Temperature and humidity data loggers can reveal problems that a visual inspection misses. Keep the records with the shipment, not in a separate office file. This improves traceability.

Track every handover. Photograph pallets before loading, after warehouse transfer, and at delivery. Check for crushed corners, broken seals, moisture marks, and loose bottles. A trained receiver should count damaged units and note the exact carton location. Small details matter.

However, tracking tools are not perfect. A sensor may be attached incorrectly, or a worker may forget one inspection. Review these failures openly. Update the packing method, handling instructions, and carrier feedback after each shipment. Quality control becomes stronger when real shipping evidence guides the next decision.

How to Ensure Bottle Quality During Shipping from China?

Control shipping conditions and track product handling before, during, and after transit.

Use controlled conditioning values as a baseline for packaging inspections: 23°C and 50% relative humidity are commonly used standard laboratory conditions for packaging evaluation. During shipment, monitor temperature, humidity, impact, and seal integrity with data loggers and inspection records. Product-specific resin, closure, and packaging specifications should always take priority.

Inspect Delivered Bottles and Resolve Quality Issues

Inspect every delivered bottle before approving the shipment. China ranked 19th in the World Bank’s 2023 Logistics Performance Index, yet transit conditions can still vary between ports, trucks, and warehouses. Record carton counts, pallet condition, seal numbers, and delivery temperature when relevant.

Open cartons from the top, middle, and bottom of the shipment. Check cracks, chips, scratches, cloudy areas, uneven walls, neck dimensions, and closure fit. Use calipers for critical dimensions and a simple leak test for filled samples. ISO 2859-1 provides a recognized sampling framework, but do not copy an AQL number blindly. The acceptable level depends on bottle use, defect severity, and customer risk.

Photograph defects beside a ruler and label each sample with the carton number. Keep damaged packaging; it may reveal compression, impact, or poor pallet stacking. ASTM D4169 can guide distribution-performance testing for future shipments. For a quality claim, send the supplier a measured defect count, sample size, photos, and batch details within the agreed reporting period. Request a written root-cause analysis and corrective action, not only replacement bottles. A credit may hide the real problem.

Review your own inspection too. Were samples taken from one pallet only? Were lighting and gauges consistent? I have seen teams reject cosmetic marks while missing loose neck finishes. That mistake is uncomfortable, but useful. Reinspect corrected goods before loading, and retain sealed reference samples for comparison.

FAQS

What materials should be checked before bottle production?

Verify resin or glass composition, batch numbers, and supplier certificates. Check the shoulder, base, and neck for consistent wall thickness. A clean surface does not prove strength.

Why is a sealed sample important?

A sealed sample becomes the approved reference for dimensions, color, closure fit, and finish quality. Compare production bottles against it before mass manufacturing. Small differences matter.

How can manufacturers detect weak bottles during production?

Inspect incoming materials, molding temperatures, cooling time, and machine settings. Check early production pieces before approving the full run. Record weight, neck finish, color, and defects hourly.

What packaging helps prevent bottle damage during transport?

Use dividers, molded inserts, or foam to stop bottle movement. Protect glass necks and bases with extra cushioning. Keep cartons away from direct floor contact. No empty space.

Can stronger packaging create new problems?

Yes. Extra cushioning can increase weight and freight costs. An overly tight carton may create pressure points. Test smaller and roomier cartons before choosing one.

Which shipping conditions should be recorded?

Record loading temperature, pallet height, carton arrangement, and seal condition. Track humidity and temperature during long routes. Carton moisture can weaken stacking strength.

How should shipment handling be documented?

Photograph pallets before loading, after transfers, and at delivery. Check crushed corners, broken seals, moisture marks, and loose bottles. Match findings with carton and batch records.

Are tracking sensors and inspection reports completely reliable?

Not always. A sensor may be attached incorrectly, and a worker may miss an inspection. Review these failures honestly, then adjust packaging and handling instructions. The process can still be imperfect.

Conclusion

How to ensure bottle quality during shipping begins with clear standards established before production. Define acceptable limits for dimensions, appearance, strength, sealing performance, and cleanliness so that manufacturers and inspectors share the same expectations. Choose durable, suitable materials and verify them through incoming checks. During manufacturing, monitor forming, molding, finishing, and closure processes, while using sampling inspections to identify defects before products leave the facility.

Protective packaging is equally important for preventing scratches, cracks, deformation, and contamination. Use properly fitted dividers, cushioning, moisture protection, and strong outer cartons designed for the shipping route. Control storage and transportation conditions, including temperature, humidity, stacking, and handling, and use tracking records to identify potential risks. After delivery, inspect the bottles promptly against the agreed standards, document any damage with photographs and inspection reports, and separate affected goods. Clear communication with suppliers and carriers can then support timely corrective action and continuous improvement.
Henry

Henry

Henry is a dedicated marketing professional with a profound expertise in the company's offerings. With years of experience in the industry, he possesses an impressive understanding of the market dynamics and consumer behaviors that drive success. Henry is committed to sharing his insights through......